Classical Nucleation Theory modified for extreme supersaturation provides a mathematical framework for predicting when ice crystals will seed in a vial headspace. This mathematical clarity is becoming increasingly vital as the pharmaceutical landscape in 2026 shifts toward highly complex protein therapeutics and personalized vaccines that require absolute structural stability. Lyophilization, or freeze-drying, has functioned as the gold standard for stabilizing these delicate molecules since its large-scale deployment during World War II for plasma preservation. However, the process has historically been plagued by a lack of control during the initial freezing phase. In a standard commercial batch containing thousands of vials, the moment of ice formation usually occurs randomly due to stochastic supercooling. This randomness creates a heterogeneous environment where some vials freeze early and others late, leading to inconsistent pore sizes across the batch. Such variability does more than just affect the visual appearance of the cake; it creates massive differences in the resistance to vapor flow during primary drying, often forcing manufacturers to extend cycle times to accommodate the slowest-drying vials. By implementing advanced controlled nucleation technologies, the industry is finally moving toward a more deterministic and efficient manufacturing paradigm that ensures every single vial follows an identical thermal trajectory.
Thermodynamics of Rapid-Depressurization Cycles
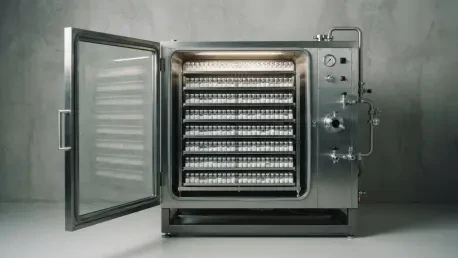
Rapid-Depressurization Controlled Ice Nucleation, frequently utilized under the ControLyo brand, leverages fundamental thermodynamic principles to achieve simultaneous ice formation throughout a freeze dryer. The operational sequence begins by equilibrating the pharmaceutical product at a temperature slightly above its freezing point, typically around 5 degrees Celsius, and then pressurizing the chamber with an inert ballast gas such as nitrogen or argon. Once the entire batch is thermally uniform, the chamber pressure is abruptly released, causing a rapid adiabatic expansion of the gas within the vial headspace. This expansion results in a sudden, localized temperature drop that exceeds the threshold required for spontaneous ice formation. Because the pressure release happens nearly instantaneously throughout the entire chamber volume, every vial experiences the same cooling stimulus at exactly the same time. The resulting cloud of ice nuclei quickly descends to the liquid interface, triggering a uniform nucleation event. This synchronization eliminates the randomness inherent in traditional cooling methods, providing a reliable foundation for the subsequent drying stages. By controlling the exact moment and temperature of nucleation, engineers can manipulate the crystal structure to favor larger, more uniform pores that facilitate faster sublimation.
The transition from a stochastic freezing process to a controlled one significantly impacts the macroscopic properties of the final drug product matrix. When ice crystals form simultaneously across a batch, the resulting solid structure exhibits a highly organized morphology that is far more predictable than what is achieved through uncontrolled cooling. In traditional freezing, high degrees of supercooling often lead to the formation of very small, dendritic ice crystals that create a tortuous path for water vapor to escape during primary drying. This high mass-transfer resistance not only extends the duration of the lyophilization cycle but can also lead to product defects like “collapse” if the temperature is not managed perfectly. In contrast, controlled ice nucleation allows for the growth of larger, more uniform ice crystals, which effectively lower the resistance to vapor flow. This reduction in resistance can decrease primary drying times by as much as 40 percent in some formulations, representing a massive increase in throughput for high-volume pharmaceutical manufacturing. Furthermore, the uniformity of the cake structure ensures that reconstitution times—the time it takes for a healthcare provider to turn the powder back into a liquid—are consistent across all vials in a given production lot.
Fluid Mechanics and Gas-Specific Dynamics
The intricate physics governing the depressurization event are rooted in the principles of reversible isentropic expansion and high-speed gas dynamics. When the exit valve of a freeze dryer is opened to initiate nucleation, the gas within the chamber moves from a state of high stagnation pressure to a lower static pressure, often reaching supersonic speeds at the point of exit. Computational fluid dynamics frameworks are essential for modeling this behavior, as they must account for the transition from choked flow to subsonic regimes. Choked flow occurs when the pressure ratio across the valve exceeds a critical value—approximately 1.89 for diatomic nitrogen and 2.05 for monatomic argon—causing the gas velocity to reach the speed of sound. During this phase, the rate of depressurization is limited by the geometry of the valve and the properties of the gas rather than the pressure differential alone. As the pressure within the chamber drops, the flow eventually becomes subsonic, and the rate of cooling begins to decelerate. Understanding these dynamics is crucial for predicting the intensity of the thermal shock delivered to the vial headspace, as even a minor deviation in the pressure release profile can lead to incomplete nucleation across the batch.
A key metric in determining the success of the controlled nucleation process is the equipment’s geometric ratio, defined as the total chamber volume divided by the effective exit area of the discharge valve. This ratio acts as a primary determinant for the pressure-time profile during the depressurization event, influencing both the depth of the temperature drop and the duration of the cooling effect. For a laboratory-scale unit like the SP Scientific LyoStar 3, the geometric ratio for nitrogen is approximately 335 meters, while for argon, it is roughly 369 meters. These values are used in conjunction with fourth-order numerical integration methods to map the transition between flow regimes and ensure that the cooling rate is sufficient to seed ice crystals. The use of argon is particularly interesting in this context because its specific heat ratio and molar mass differ from nitrogen, leading to different expansion characteristics. By solving the energy and momentum equations for these specific gases, researchers can optimize the starting pressure and shelf temperature to ensure that the nucleation “cloud” is generated with enough density to reliably contact the liquid surface in every vial, regardless of their position on the shelf.
Computational Modeling of Multiphase Interactions
To accurately capture the complexity of the nucleation event, modern engineering approaches utilize multiphase computational fluid dynamics that integrate Eulerian and Lagrangian frameworks. The Eulerian phase handles the continuous gas mixture of water vapor and the inert ballast gas, employing conservation equations for mass, momentum, and energy. Because the conditions during rapid expansion involve extreme temperature gradients and high pressures, the ideal gas law is often insufficient for maintaining accuracy. Instead, the Soave-Redlich-Kwong real gas equation of state is applied to account for the non-ideal behavior of the gases and to provide a more rigorous prediction of the vapor-liquid equilibrium. This level of detail is necessary to understand how the gas density and thermal conductivity change in real time as the pressure drops. The model must also account for the geometry of the vial, the partially seated stopper, and the meniscus of the liquid product, all of which influence the flow patterns and temperature distribution within the headspace. By simulating these variables, researchers can visualize the buoyancy-driven flows and pressure gradients that ultimately dictate where the ice crystals will form.
The discrete phase of the simulation focuses on the life cycle of individual water droplets and ice crystals using a Lagrangian tracking approach. These particles are modeled as discrete parcels that move through the Eulerian gas field, influenced by a balance of forces including gravity, drag, and pressure gradients. The modified Classical Nucleation Theory is the primary driver for predicting the birth of these nuclei, determining exactly when the local supersaturation levels are high enough to overcome the energy barrier for phase change. Once formed, the parcels are tracked as they exchange heat and mass with the surrounding gas. Their transition from a liquid droplet to a solid ice crystal is governed by a survival temperature model, which incorporates the high cooling rates observed during expansion—often reaching minus 40 Kelvin per second. This simulation capability allows engineers to predict the trajectory of the ice crystals, ensuring they possess enough momentum to overcome the upward-moving vapor and reach the liquid surface. Without this granular level of tracking, it would be impossible to determine why certain process parameters fail to induce nucleation while others succeed, making the CFD model an indispensable tool for process optimization.
Empirical Validation and Gas Selection Strategies
The development of these complex computational models would be purely theoretical without rigorous empirical validation conducted in controlled laboratory environments. Using ultrapure water as a standardized test medium, researchers perform extensive validation trials in specialized freeze dryers to verify the accuracy of the CFD predictions. These trials typically involve a Design of Experiments framework, such as Latin hypercube sampling, to systematically explore the operational boundaries of the equipment. By varying the initial discharge pressure and the shelf temperature across a wide range, engineers can identify the exact conditions where a batch transitions from partial to complete nucleation. Data from these experiments, often collected using high-speed thermal sensors and hexagonal vial arrays, show a remarkably high correlation with the simulation results. In most cases, the CFD model accurately predicts the success rate of the batch within a margin of only a few vials, with minor discrepancies usually attributed to unavoidable surface-level stochastic events. This validation process confirms that the digital twin of the freeze-drying process can reliably substitute for expensive and time-consuming physical trials during the early stages of cycle development.
A significant outcome of recent research is the realization that the choice of ballast gas plays a critical role in the efficiency of the nucleation process. While nitrogen is the most common choice due to its low cost and availability, argon has demonstrated superior performance in specific vial geometries and low-pressure scenarios. The primary reason for this advantage lies in the lower thermal conductivity of argon compared to nitrogen. During the depressurization event, the temperature difference between the cold headspace gas and the relatively warm vial walls creates buoyancy-driven currents that can push newly formed ice nuclei away from the liquid interface. Because argon is less thermally conductive, these buoyancy forces are dampened, allowing the pressure-driven flow to maintain better control over the particle trajectories. Consequently, argon can achieve 100 percent batch-wide nucleation at discharge pressures that are significantly lower than those required for nitrogen. This finding is particularly important for manufacturing facilities that operate older equipment with pressure limitations or for pharmaceutical products that are sensitive to high-pressure environments. Selecting the right gas is no longer just a matter of logistics; it is a strategic decision that directly impacts the robustness of the stabilization process.
Industrial Scale-up: Translating Lab Data to Production
The transition from laboratory-scale development to production-scale manufacturing is perhaps the most challenging aspect of pharmaceutical engineering, particularly when dealing with high-speed thermodynamic events. The equipment geometric ratio, V/Ae, remains the most critical scaling factor in this transition. In large industrial freeze dryers, the chamber volume increases exponentially, but the size of the discharge valves often does not scale at the same rate due to mechanical and cost constraints. This leads to a higher geometric ratio in production units, which inherently slows down the rate of depressurization compared to smaller lab units. According to the CFD models, this slower pressure drop means the adiabatic cooling is less intense, potentially shifting the nucleation boundary and requiring lower shelf temperatures to achieve the same result. For instance, an increase in the V/Ae ratio from 335 to 355 meters might necessitate a shelf temperature adjustment of several degrees to maintain the integrity of the nucleation event. Understanding these shifts through mathematical modeling allows process engineers to proactively adjust their parameters during technology transfer, ensuring that the “quality by design” established in the lab is maintained at the commercial scale.
The ultimate goal of using these advanced modeling tools is to create comprehensive response surface maps that define the safe operating space for a specific product and piece of equipment. These maps provide a visual and mathematical representation of the probability of successful nucleation, allowing manufacturers to “design in” quality from the very beginning. By identifying the specific operational boundaries—such as the minimum pressure required at a given temperature—companies can ensure that their processes are inherently robust against minor fluctuations in environmental conditions or equipment performance. This predictive approach to lyophilization represents a major departure from the traditional trial-and-error methods that have dominated the industry for decades. As we look toward the future of pharmaceutical manufacturing in 2026 and beyond, the integration of real gas thermodynamics, multiphase CFD, and standardized scaling factors will continue to drive down costs and improve the reliability of life-saving therapeutics. The ability to suppress product variability through controlled ice nucleation is no longer a luxury; it is a fundamental requirement for the next generation of precision medicine, ensuring that every patient receives a drug of the highest possible quality. This research has successfully established the necessary framework to move these high-tech stabilization methods into the mainstream of global drug production.