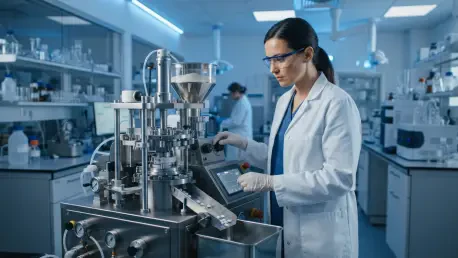
The ability to optimize tabletting processes using only small quantities of materials is a critical advantage for pharmaceutical companies navigating tight development timelines. As the pharmaceutical industry continues to evolve in 2026, the demand for sophisticated Contract Development and Manufacturing Organizations that can handle complex oral solid dosage forms has intensified significantly. Ardena has addressed this specific market challenge by installing a KORSCH STYL’ONE Evo compaction simulator at its primary research headquarters in Ghent, Belgium. This strategic investment is designed to bridge the technical gap between initial laboratory-scale formulation and the rigorous requirements of industrial-scale manufacturing. By utilizing a technology platform that precisely replicates the compression profiles of industrial rotary tablet presses, scientists can now assess powder properties with unprecedented accuracy. This transition to a data-driven development model allows for a more reliable scale-up process, ensuring that drug candidates move into clinical trials with fewer mechanical delays and improved stability.
Advanced Methodologies in Pharmaceutical Scaling
Mechanical Profiling through Compaction Simulation
The implementation of the KORSCH STYL’ONE Evo provides a highly versatile platform that mimics the mechanical stresses found in high-speed production environments. This simulator is essential for understanding how various active pharmaceutical ingredients and excipients behave under extreme pressure, which is a key factor in ensuring consistent tablet quality. By using minimal quantities of material, the system allows for the detailed characterization of compaction energy, elasticity, and solid-state properties without the high costs associated with large-scale pilot runs. This level of precision is particularly important for specialized medicines where the chemical stability and physical robustness of the dosage form are paramount. Furthermore, the integration of advanced sensors allows researchers to generate comprehensive compression profiles that can be applied to various tablet press models across different manufacturing sites. This capability ensures that the formulation developed in Belgium remains consistent and effective when transferred to international production facilities for commercial distribution.
Mitigation of Production Risks and Material Waste
Beyond basic formulation development, the use of compaction simulation is a powerful tool for the early identification of common manufacturing defects such as capping, lamination, and sticking. These issues often arise during the transition from a laboratory setting to a high-speed industrial press, potentially leading to significant production losses and project setbacks. By simulating these industrial conditions early, the engineering team can resolve potential mechanical failures before they impact the broader supply chain. This proactive risk management is vital for maintaining tight clinical timelines and reducing the overall environmental footprint by minimizing material waste. The ability to troubleshoot these problems at the gram scale ensures that the final manufacturing process is both robust and commercially viable. Consequently, the organization can provide clients with a higher degree of confidence that their drug products will maintain structural integrity throughout the manufacturing lifecycle, regardless of the complexity of the chemical composition.
Global Strategic Growth and Bioanalytical Support
The broader strategic expansion in 2026 showcased a commitment to providing integrated pharmaceutical solutions across the entire development spectrum. While the Ghent facility focused on refining oral solid dosage forms, the opening of a new bioanalytical laboratory in Somerset, New Jersey, significantly bolstered the ability to support clinical trials in North America. Additionally, significant progress was made in the field of nanomedicine, particularly in supporting the development of the anticancer candidate PRD-101. These initiatives highlighted an organizational shift toward using data-driven insights to manage complex drug formulations effectively. By expanding the international footprint and adopting high-precision simulation tools, the organization successfully bridged the technical hurdles that often slowed the path from discovery to the clinic. These initiatives ensured that innovative therapies were not only scientifically sound but also scalable and ready for global markets, thereby establishing a more efficient framework for future development projects.